
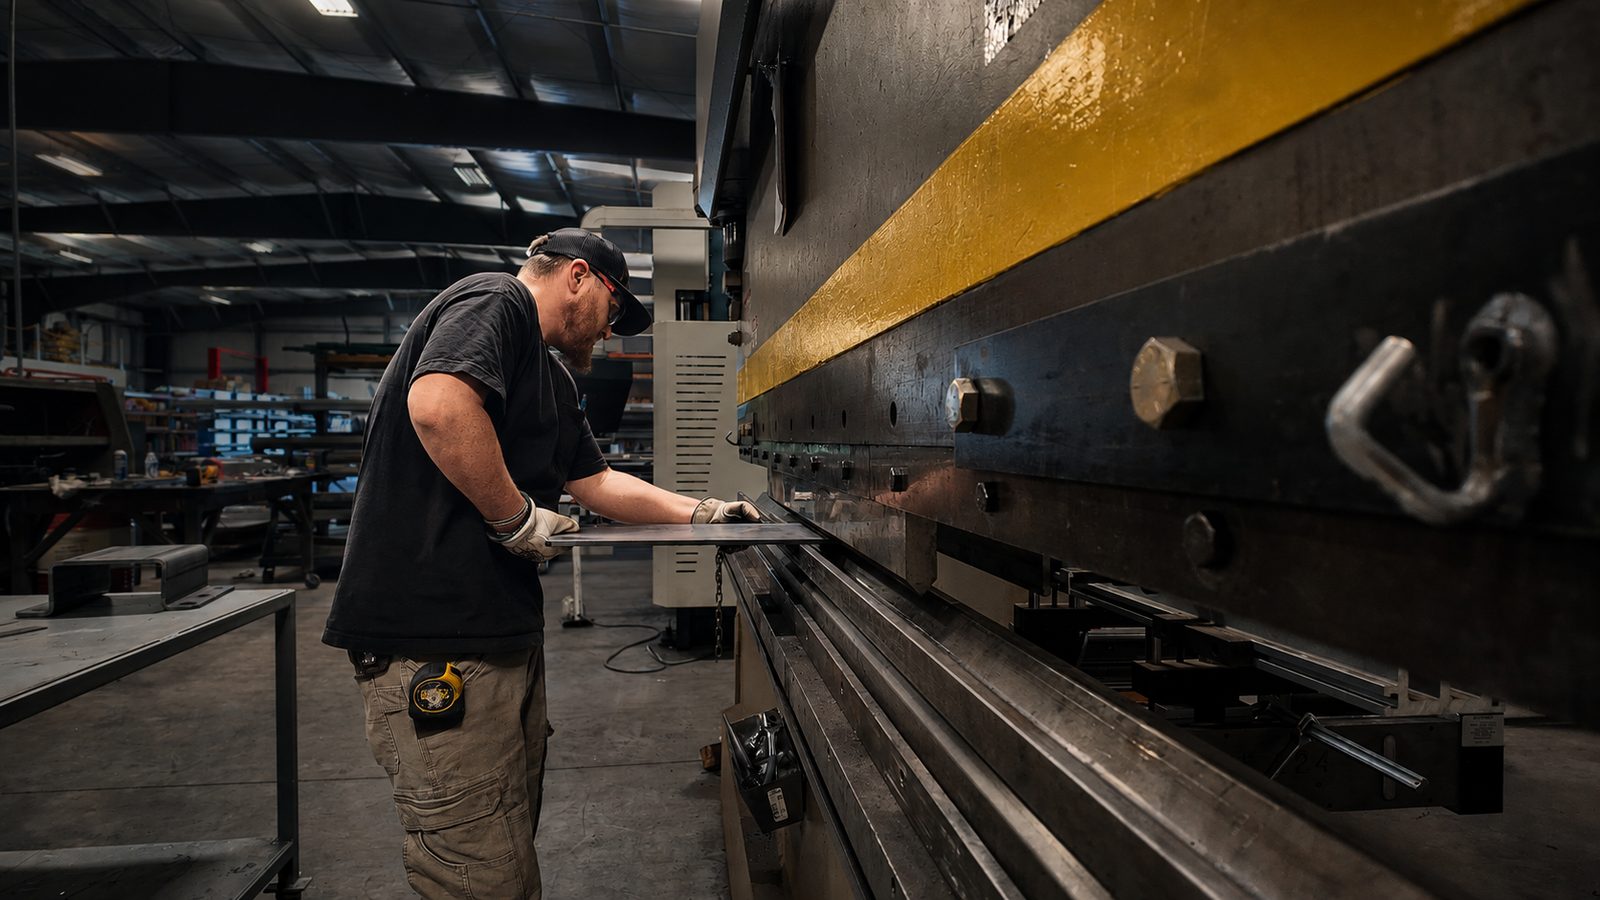
Press brakes
165-ton Pacific and 150-ton CNC Durma Precision. Heavy-plate capacity and programmable repeatability on the same floor.
CNC machining, laser cutting, press brake forming, saw cutting, welding, assembly, powder coating, and metal finishing, including quick turnaround manufacturing and low-high volume production parts.
A part usually needs several of these in sequence. Running them under one roof is the point.
Clean, accurate profile cutting for sheet and plate.
Bar, tube, and structural stock cut to length.
Flat blanks cut to size, ready for downstream forming.
165-ton Pacific and 150-ton CNC Durma Precision brakes.
Machined components produced to your print.
TIG, MIG, Flux Core, and Stick brought onto the production floor.
Multi-part assemblies built up and delivered ready to install.
Durable powder finish applied to finished parts.
Surface preparation and finishing, plus an in-house air spray paint booth.
Panels, enclosures, brackets, and multi-part assemblies manufactured to your printually have.
Finished parts crated and shipped anywhere in the country.
Short-run work handled without a production-line lead time.
Small quantities treated as real production, not an inconvenience.

Quick turnaround manufacturing and low-high volume production parts are stated capabilities, not exceptions we squeeze in. If you need ten of something rather than ten thousand, that is a job we are set up to take.
165-ton Pacific and 150-ton CNC Durma Precision. Heavy-plate capacity and programmable repeatability on the same floor.

Bend sequences programmed at the control, so the tenth part matches the first.

A 10′ × ¼″ shear, multiple sawing and cutting equipment, and multiple manual machining equipment.

CNC laser and plasma cuttinging, nesting software, and an in-house air spray paint booth.

Laser cutting runs off the same DXF, SVG, and vector files we nest for plasma. The profile is cut in-house, and the blank goes straight to forming, machining, welding, and finishing without leaving the building or changing vendors.
Steel plate and sheet cut in our Winchester shop, photographed on the machine and on the bench.

Sheet stock squared up on the slats and the head brought down to height before the cut starts.

The cut running under power, with the spark stream carrying the melt clear of the kerf.

Looking straight down the head as it tracks the profile across the sheet.

Customer artwork brought in as a vector file and cut as drawn, detail and all.

Material staged and the head parked between nests while the next sheet is loaded.

Finished profiles left in the skeleton, ready to be broken out and sent on to forming.
STEP, DWG, DXF, or PDF in, for laser, plasma, and saw cutting. Nesting software sets the material layout.
Laser cutting, CNC plasma, saw cutting, and blanking.
Press brake forming, tube bending, and CNC or manual machining.
TIG, MIG, Flux Core, or Stick, then built up into assemblies.
Powder coating, metal finishing, and air spray booth before it ships.